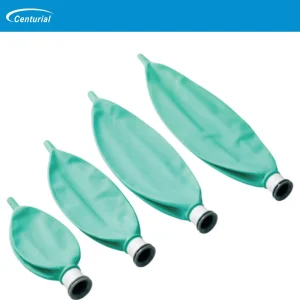
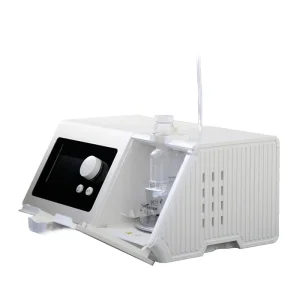
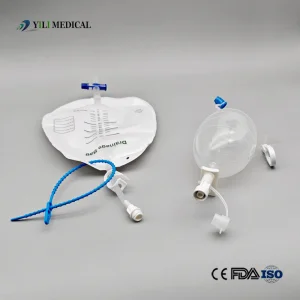
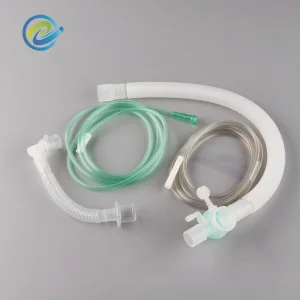
Shanghai Ryu Medical Co., Ltd. has established itself as a cornerstone in the medical manufacturing landscape. With over 10 years of intensive R&D and clinical application experience, we bridge the gap between high-efficiency Chinese manufacturing and the stringent requirements of global healthcare systems in Europe, Africa, Asia, and America.
Our commitment to E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) is reflected in our rigorous QC processes. By maintaining direct control over production lines and partnering with 5+ strategic facilities, we ensure that every tube, bag, and respiratory component meets CE and ISO international quality benchmarks.
The global fluid transfer solutions market is evolving towards "smart clinical integration." From intelligent tube labeling to precision-monitored ICU diuresis systems, modern healthcare providers demand devices that reduce human error and improve patient outcomes. China's manufacturing ecosystem now leads in "Rapid-Response Production," enabling us to scale from prototype to mass production for global procurement needs efficiently.
A: We implement a multi-tiered QC strategy. Every batch undergoes stress, integrity, and compatibility testing to meet ISO standards.
A: Yes. With over a decade of experience, our technical team works directly with clinical partners to refine designs for specialized surgical or diagnostic applications.
 Ryu Medical